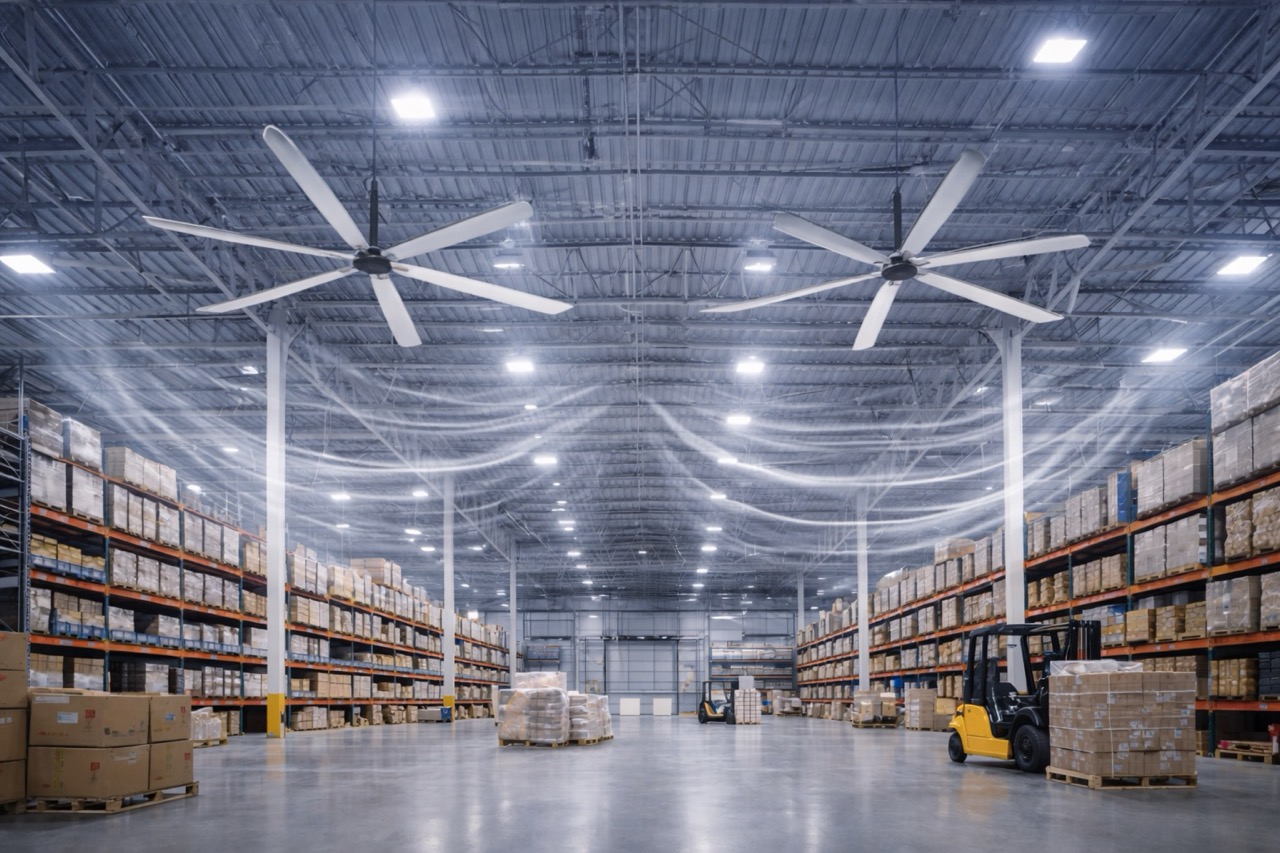
WCSIPL delivers specialized HVAC systems for half-frozen and ready-to-eat product facilities — maintaining strict temperature, humidity, and air quality to ensure food safety, extend shelf life, and meet FSSAI and global regulatory standards.
Half-frozen and ready-to-eat (RTE) food products occupy a critical temperature zone — typically between -2°C and +8°C — where even minor deviations can trigger microbial growth, texture degradation, and shortened shelf life. These products require not just cooling, but precisely controlled environments with tight temperature uniformity, regulated humidity, and superior air cleanliness.
WCSIPL engineers HVAC systems specifically designed for the unique demands of half-frozen and RTE food production and storage — integrating precision refrigeration, humidity control, HEPA filtration, and validated temperature mapping to create environments that protect product quality from production to dispatch.
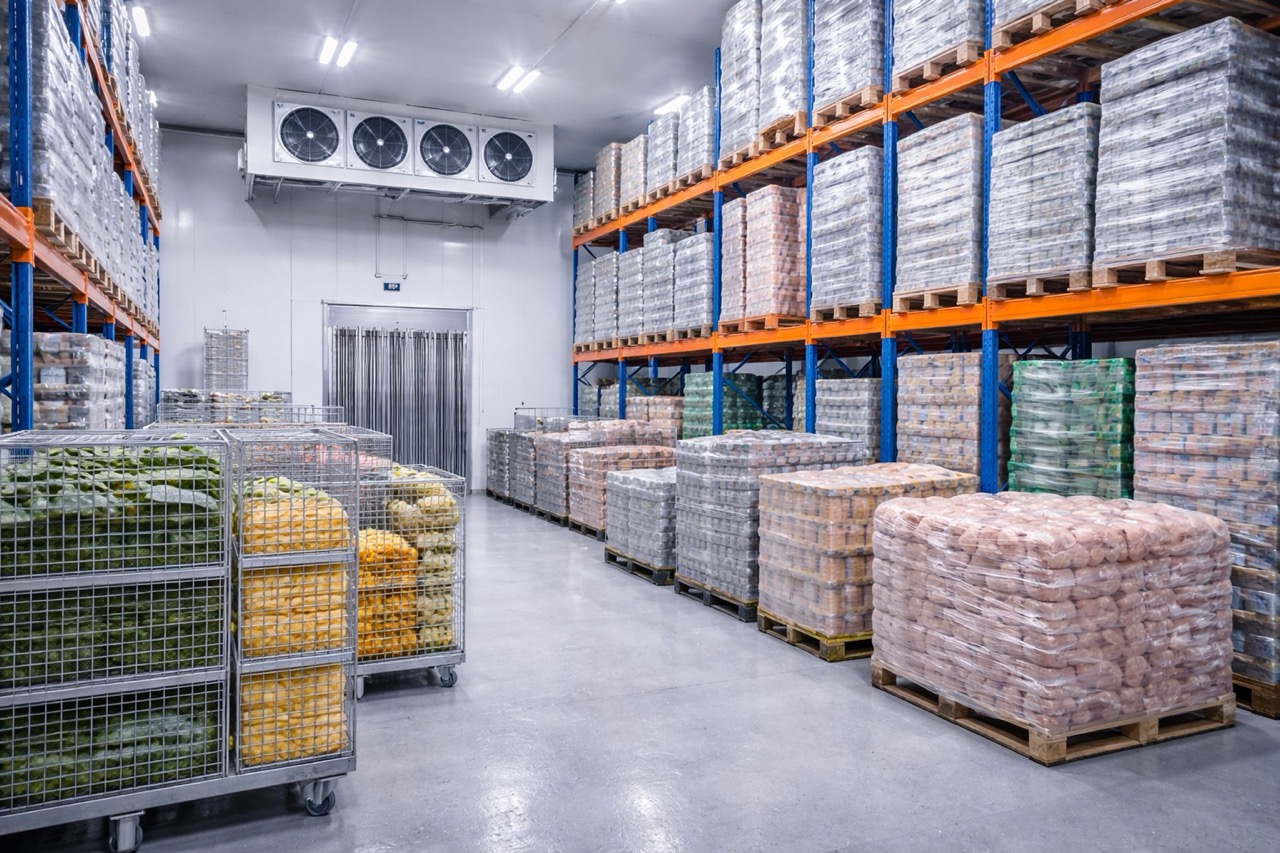
Standard air conditioning cannot deliver the temperature precision, humidity control, and air quality that half-frozen and RTE food products demand throughout the supply chain.
Half-frozen products must be maintained between -2°C and +4°C, while RTE products typically require +2°C to +8°C. A fluctuation of even 2–3°C can cause partial thawing, ice crystal growth, texture loss, or accelerated bacterial growth — leading to product rejection and financial losses.
Uncontrolled humidity causes condensation on product surfaces and packaging, promoting mould growth and label damage. Conversely, excessive dryness causes surface dehydration and weight loss. Half-frozen and RTE environments must maintain relative humidity between 85–95% — a range standard HVAC systems cannot reliably hold.
FSSAI, EU Regulation 852/2004, US FDA 21 CFR Part 110, and HACCP protocols mandate documented temperature control, continuous monitoring, alarm systems, and validated environmental conditions for RTE and chilled food facilities. Non-compliance results in product holds, recalls, and licence suspension.
Every system component is engineered to maintain precise, uniform, and validated environmental conditions throughout the production and storage cycle.
Multi-stage refrigeration systems with PID-controlled expansion valves and modulating compressors maintain set-point temperatures within ±0.5°C accuracy. Redundant compressor configurations and automatic switchover ensure uninterrupted cooling even during equipment maintenance or partial failures — critical for 24/7 cold chain operations.
CFD-optimized duct design with perforated ceiling diffusers and low-velocity supply air ensures uniform temperature distribution across the entire storage zone — eliminating hot spots, cold spots, and temperature stratification that can cause inconsistent product quality in different areas of the same room.
Dedicated humidification and dehumidification systems integrated with the AHU maintain relative humidity within the precise 85–95% band required for half-frozen products. Intelligent dew-point control prevents condensation on ceilings, walls, and product surfaces while avoiding surface dehydration and weight loss.
Multi-stage air filtration with HEPA (H13/H14) final filters removes 99.97% of particles ≥0.3 microns — including bacteria, mould spores, and dust. Optional UV-C sterilization in the supply airstream provides additional microbial control, critical for RTE products that do not undergo further cooking before consumption.
SCADA-integrated temperature and humidity monitoring with calibrated sensors at multiple points throughout each zone provides real-time visibility. Multi-level alarm systems — local audible/visual, SMS/email alerts, and BMS integration — ensure immediate response to any deviation, with automatic data logging for regulatory compliance documentation.
Intelligent defrost control with hot-gas and electric defrost options minimizes temperature rise during coil defrost cycles — typically keeping product zone temperature deviation below 1°C. Staggered defrost scheduling across multiple evaporator coils ensures continuous cooling capacity is always available in the room.
Our precision climate systems deliver measurable improvements in product safety, shelf life, energy efficiency, and regulatory compliance.
Precise temperature and humidity control slows microbial growth and enzymatic degradation, extending product shelf life by 30–50% compared to standard cold storage — reducing waste and improving profitability.
Uniform temperature distribution eliminates hot spots that cause partial thawing, ice crystal reformation, and texture degradation — ensuring every unit meets the same quality standard from first to last pallet.
Continuous monitoring with data logging, validated temperature mapping, and alarm systems meet FSSAI, HACCP, EU, and FDA requirements — simplifying audits and eliminating compliance-related product holds.
VFD-driven compressors and fans, EC fan motors, floating head pressure control, and intelligent defrost management reduce energy consumption by 25–35% compared to conventional cold room systems.
All AHU components, ductwork, and coils feature food-grade construction with cleanable surfaces, drainable configurations, and no microbial harbourage points — meeting hygienic design standards for food production environments.
Elimination of temperature excursions, condensation damage, and dehydration shrinkage directly reduces product rejection rates and waste — delivering rapid ROI through avoided losses alone.
Our precision climate control systems serve every temperature-critical zone in the half-frozen and ready-to-eat product workflow.
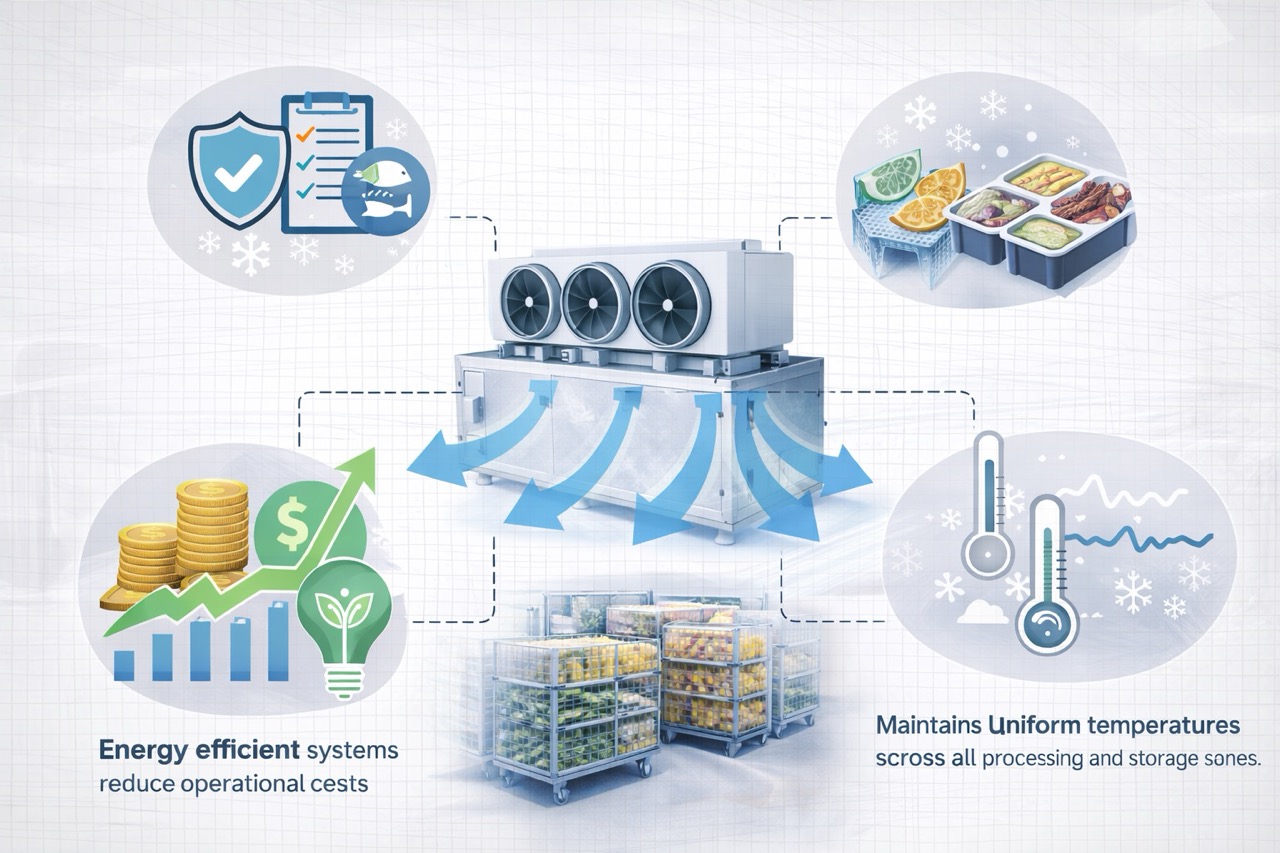
Our specialized cold chain HVAC expertise and turnkey execution capabilities make us the ideal partner for temperature-sensitive food facilities.
Deep experience in HVAC for food processing, cold storage, and temperature-controlled environments since 2008 across India.
Proven ability to maintain tight temperature tolerances with validated mapping — meeting the most stringent food safety requirements.
From thermal load calculation and system design to fabrication, installation, commissioning, and validation — everything under one roof.
Dedicated cold chain service teams with rapid response for emergency breakdowns, preventive maintenance, and calibration services.
Answers to common queries about HVAC systems for half-frozen and ready-to-eat food product facilities.
Get a free thermal assessment and custom-engineered HVAC proposal for your half-frozen or RTE product facility. Our cold chain specialists will design a system that meets your exact temperature, humidity, and compliance requirements.